Guangdong Petrochemical Fired Heater Project

Project Summary
| Item | Details |
|---|---|
| Industry | Petrochemical |
| Steel Tonnage | 1000 t |
| Material Grade | Q355 |
| Project Year | 2021 |
| Delivery Time | 1 month |
| Fabrication Scope | Shop detailing, steel fabrication, welding |
| Surface Treatment | Sa 2.5 |
Project Background
About This Project
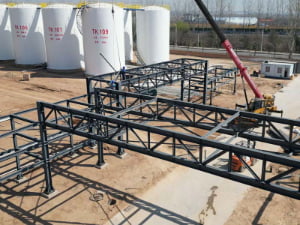
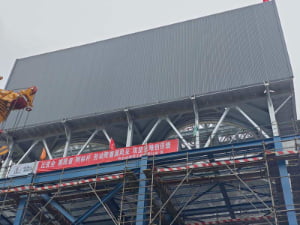
In the Guangdong Petrochemical Project, our team delivered a custom steel structure solution for the convection section of a box-type fired heater. The project utilized approximately 1,000 tons of high-strength steel to construct a robust support frame capable of withstanding extreme high-temperature and heavy-duty conditions. The steel structure was precisely engineered and fabricated to meet the stringent requirements of industrial furnace systems, ensuring long-term stability, durability, and safe operation under demanding operational conditions.
Client Requirements
What the Client Needed
- 12.1 All steel structures of this unit (excluding profiled steel sheets) shall undergo coating treatment.
- 12.2 The corrosion protection for steel structures is designed to withstand the corrosive atmosphere of a petrochemical environment.
- 12.3 Steel structural components that have passed fabrication quality inspections shall undergo rust removal prior to coating; the surface rust removal methods and grades shall comply with the requirements specified in the table below. Anti-rust primer shall be applied promptly after surface preparation, with an interval not exceeding 4 hours.
Fabrication Process
Fabrication Process
Standard production workflow from detailing to delivery.
Standards & Delivery
Quality Assurance to Final Delivery
Quality Control
Material traceability was maintained according to project requirements. Raw materials were inspected before production, and welding and surface treatment were checked after fabrication. Third-party inspection was arranged when required to support compliance with project quality requirements and EN standards.
Surface Treatment
Surface derusting: The minimum surface preparation grade shall be Sa 2.5 for frame columns and beams, bracing members, and equipment beams. Coating System: Two coats of epoxy zinc-rich primer, with a minimum dry film thickness of 70 μm; one coat of epoxy micaceous iron oxide intermediate paint, with a minimum dry film thickness of 60 μm; and two coats of acrylic polyurethane topcoat, with a minimum dry film thickness of 70 μm. The resulting total dry film thickness shall be 200 μm.
Packing & Delivery
During packing, each steel component was clearly marked for identification to facilitate installation at site. Timber supports and protective spacers were applied at bundling points to protect the painted surfaces from damage during handling and transportation.
Project Photos
Fabrication Documentation
Visual documentation of key fabrication stages and quality milestones.
-
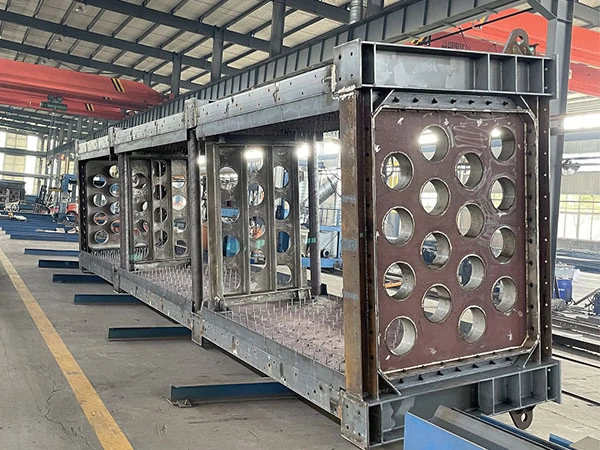
Welding of Structural Members
Related Products
Products Used in This Project
More Projects
Explore Our Work
Partner With a Reliable
Steel Structure Manufacturer
Reduce project risks through proven fabrication quality and international compliance. Send a short inquiry and our engineering team will follow up.
EN 1090 EXC3
Certified Quality Standard
Fast Response
Engineering team follow-up
50,000+ Tons/Year
Industrial-scale production capacity
Global Delivery
Middle East, SE Asia, Europe